 Produuz.it Docs
Appearance
Mobi One
The Mobi One (by H&M) is an automated timber wall panel processing machine. It handles the entire panel manufacturing process — framing, nailing, milling, sawing, drilling, and gluing — in a single station.
Overview
The Mobi One is set up as a machine setup linked to a station of your production line. produuz.it then writes the machine files for the zones that station produces. See How a file is made.
There are two versions:
- Mobi One V1 — generates MOB v1 files.
- Mobi One V2 — generates MOB v2 files, and also Panel BTLx files.
Processing Units
The Mobi One can be equipped with various processing units depending on your configuration:
| Unit | Function |
|---|---|
| Framing | Processes frame members (studs, top/bottom plates) |
| Nailers | High-speed pneumatic nailers for fastening cladding and battens |
| Screwers | Mechanical screw drivers |
| Miller/Router | Spindle for routing openings, cutouts, and milling operations |
| Drill | Multi-spindle or single-head drilling |
| Saw | Cross-cutting blade for transverse cuts |
| Gluing | Adhesive application system |
Configuration in Produuz.it
Machine Setup
In Production Settings > Machine Settings, create a setup with the model H&M Mobi One V1 Station or H&M Mobi One V2 Station, and link it to its station in Production lines. Give each station its own setup, even when two machines are identical.
The setup window has four tabs:
- General — the name and the model.
- Machine file — the machine's own configuration file: XML for a V2, a text file for a V1. Upload it before anything else. It declares which tools and units the machine has, and so which tools the report form offers and which operations can be written. The Current machine file card says when it was read. Upload it again whenever the machine changes. Without it, files cannot be generated.
- Machine setup — the settings below.
- MOB v2 panel file (or MOB v1 panel file) — the default job options, used to fill in the report form. See Job Settings.
The Machine setup tab holds:
- Switch direction X-axis — inside, outside or none. Forces the face the station reads the panel from, whatever the starting side says. Leave it on none unless the station comes out mirrored left to right.
- Switch direction Y-axis — Turns the panel over its length, so the top rail becomes the bottom rail. Use it when the station comes out upside down.
- Machine zero — The corner the machine measures from: File info (the default, read from the configuration file), top right, top left, bottom right or bottom left. At the moment only the left or right part of the choice moves the coordinates; top or bottom only changes the Machine Zeros line in the file header. The value of the station that produces zone -1 or 1 is the one used.
- Max Wall Length for X axis — The longest panel the machine takes, used when the job trims operations. Leave it empty to use the length of the configuration file.
- Blocker Height X / Y — The height of the table stops, used by the shift.
- Nailing matrix — Customize nail patterns by beam size. The Nailing Matrix by Beam Size item in the Framing section opens its own window, which holds the matrix and the three settings below; Apply writes them back into the setup, which is saved with the setup's own Save. Each beam size row sets the top/bottom padding and the number of nails. The beam size is the height of the stud where it meets the rail. Rows are kept sorted by beam size when the setup is saved.
- Nailing matrices by part class — The matrix window can hold one whole matrix per part class: the matrix by beam size, the nail columns by beam width and their two range switches, all of them per class. Pick Default or a class at the top of the window; add a class with the field beside it, choosing one of the classes of your parsing setups or typing a new name. A stud whose class has a matrix is nailed by it; a size or width with no row in that matrix falls back to the default matrix, and then to the automatic nailing. This is how a panel that mixes I-beams and solid studs of the same height gets two nails on the I-beams and five on the studs. See: IFC Parsing Setup
- Nail columns by beam width — Next to the matrix, a second table decides how many columns of nails a stud gets from its width: set No of Columns to 2 or more and Column Spacing to the horizontal distance between columns, per beam width. The machine file then repeats the nail row at each extra column position. A width that is not in the table gets a single column. Its rows can also be read as width ranges with Nail columns rows are width ranges, exactly like the size ranges of the matrix, and they are kept sorted by width as well. The window that holds both tables shows a preview: type a beam height and width, and optionally a part class, and it draws the stud's joint with the nails the machine would drive, saying which matrix row or range answered, or that the automatic nailing applies, and warning when a column would fall outside the stud. The columns are drawn where the machine drives them: the first one 22 mm from the stud's edge (the nailer's offset from the X written in the file, which centres it on a 44 mm stud), the next ones one spacing further each.
- Nailing matrix rows are size ranges — Off by default, so each row applies to the exact beam size written in it. When on, every row is the start of a size range that runs up to the next row (the last row covers everything above it): rows at 89, 120 and 160 nail 89-119, 120-159 and 160 and up, instead of needing one row per millimetre. Sizes below the first row stay outside the matrix and get the automatic nailing.
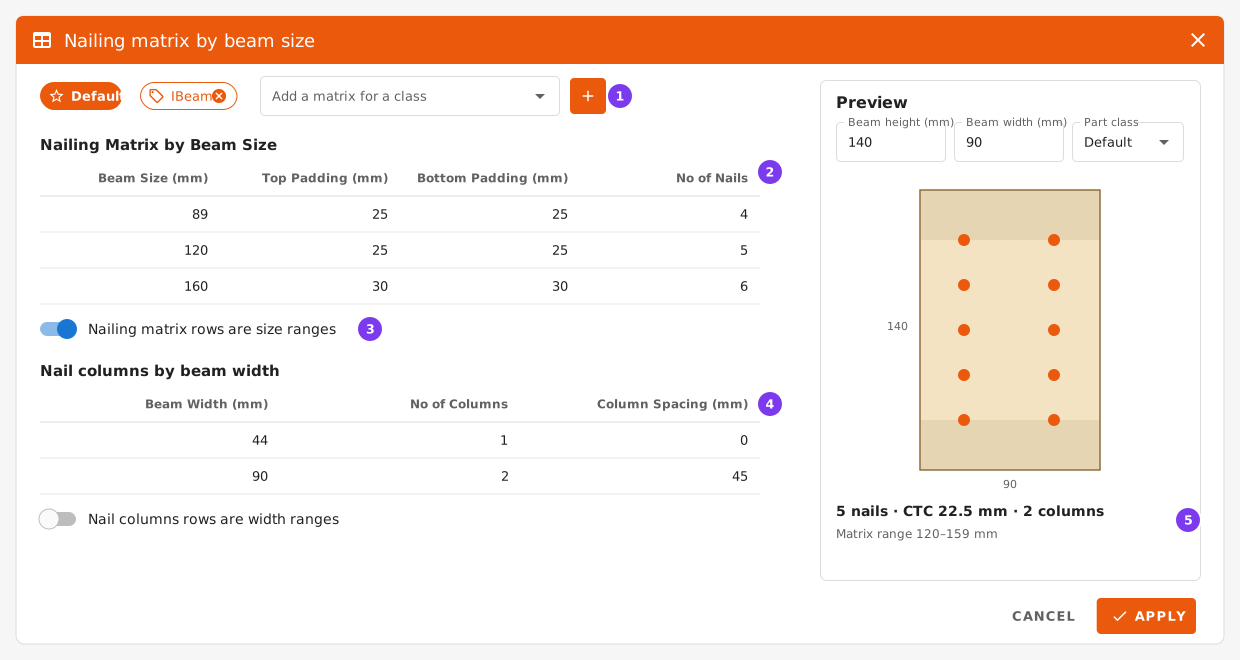
- Default and one matrix per part class. Add a class with the field beside them.
- The matrix by beam size: padding and number of nails.
- Read the rows as size ranges.
- The nail columns by beam width.
- The preview: the joint as the machine nails it, and the row or range that answered.
Processing thresholds — Minimum mill radius, CTC distances, and other tolerances.
Treat extra woods as normal frame woods — Off by default. When off, extra woods (extra top/bottom wood and extra frame wood profiles) are handled as reinforcements: the extra rails are placed as ordinary horizontal pieces and get ledge nailing. When on, they are handled exactly like the rest of the frame: extra rails become top/bottom rails, they are nailed with the standard framing matrix, and they are included in flooring.
This option is set per station, so each machine in the production line decides on its own. The typical use is a line where the frame station builds the frame without the extra pieces (option off) and a later station receives the panel with them already mounted (option on).
A station with the option on also measures the panel from a different corner: because the extra pieces are already mounted, the panel is physically bigger, so its zero is the corner of the frame including them. Stations with the option off keep measuring from the structural frame, and an extra piece that sticks out lands on negative coordinates — the same as before.
Angular nailing — Off by default. For machines equipped with a tilting nailer unit: nailer codes in the file are written with 4 digits (
00,10or20in front of the tool number). Nailing along the panel contour, around windows and in the middle of a plate stays straight (00+ tool). At a joint between two plates, the nail row on the left side of the joint gets10+ tool and the one on the right side gets20+ tool, so each row is driven at an angle into the shared wood. Every zone also gets a Nail Context drawing with the operation drawings, showing how each nail line was classified (contour, window, plate joint or plate face).SVG Drawings — All on by default. One switch per operation drawing generated with the machine files: Framing nails, Frame Glueing, Operations (plates nailing), Glueing, Bricks, Isolation, Battens, Batten Intersections, Plates Layout and the Nail Context debug drawing. Turn off the ones you don't use to skip generating them — the machine files themselves are not affected. In a production line with several stations, the switches of the machine that owns zone 0 (the frame) apply to the whole line.
Job Settings
The job options are chosen for each file, in the Station Job Options block of the report form: starting side, shift mode, trimming, frame nailing matrix, twin nailing height, mill and saw directions and tools. Every option is explained on the MOB v2 page.
The spacing of plate nail lines is not a job option: it comes from the model, or from Default value for CTC in plates nailing in the Cladding section of the machine setup.
INFO
Save your usual job options as defaults on the machine setup, in the tab of each file type it produces (for a Mobi One V2: MOB v2 panel file). They fill in the report form each time.
The zone 0 station decides for the line
The Production starting side and Shift mode of the station that produces zone 0 apply to the whole line. Set them there.
Generating Machine Files
- Open Production files in the Files section of the left menu, in your project (or in company-wide mode, if your company works by dates).
- Click New file and pick MOB v1 Machine File (or MOB v2 Machine File) as the Report Type.
- Choose the production line and select the assemblies to process.
- Adjust job settings if needed.
- Click Submit to generate.
The output is a ZIP file with one machine file per design (.mob for V1, .mob2 for V2), an orientation report for each one, and the operation drawings. See Output.
When a file comes out mirrored
First check that the panel itself is right: in the 3D viewer, Front must show the outside face with the bottom rail at the bottom. If it does not, the cause is in the zones or the rails of the model. See Panel Sides and Coordinates.
Then check these in order:
- The
.orientation.txtfile next to the machine file in the ZIP. It lists, per station, the zones, the machine zero, the starting side, the orientation settings, and which station owns zone 0. - The starting side of the station that owns zone 0. It applies to the whole line.
- Machine zero, on the station that produces zone -1 or 1. With File info, check that the configuration file is the current one: the Current machine file card of the Machine file tab says when it was read.
- Mirrored left to right: Machine zero and Switch direction X-axis.
- Upside down: Switch direction Y-axis. On a Frame Station, the face inversions. See Frame Station.
- Station order: when two stations produce zones -1 or 1, the later one sets the machine zero for both.
Linking to Production
The operation drawings made with each report are added to the panel and shown to production workers behind the MOB2 button of the Viewer: nailing, milling and drilling order, plates layout and the other drawings switched on in SVG Drawings. Each new report replaces them. The machine files themselves are downloaded from Production files.